Hey guys, let’s cut to the chase if you’ve ever dealt with wedge wire filter screens—you know those slotted, precision-made metal screens that keep grains, chemicals, wastewater, even sweet stuff from clogging up operations. I’ve been in this game for 12 years, running a wedge wire filter screen supplier, and I get so many questions that boil down to one: how does wire tension even matter for structural integrity? Most folks think tension is just for keeping a guitar string tight, but no—this stuff is make-or-break for your screen lasting 6 months vs. 6 years, or failing mid-batch and costing you thousands in downtime. Let’s break this down like we’re chatting over coffee, no boring engineering jargon that makes you zone out. Wedge Wire Filter Screen
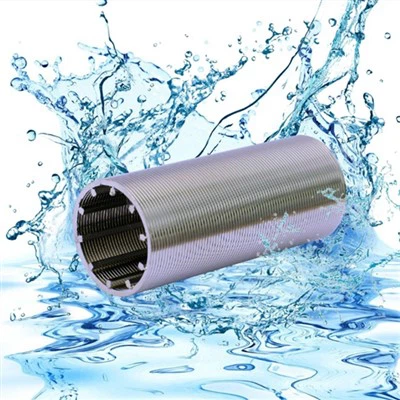
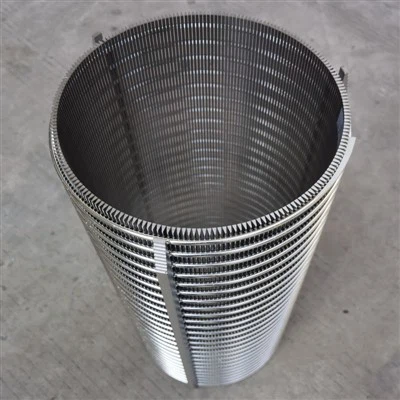
First, let’s remember what a wedge wire filter screen is at its core. We take V-shaped wedge wires (that’s where the name comes from) and connect them to support rods, right? The gaps between those wedge wires are super precise—like, sometimes 0.1mm or even smaller—so they catch the crud you don’t want while letting the good stuff flow through. The tension we’re talking about here is how much stretch or pull is put on those individual wedge wires before they get welded to the support rods. I know some new guys in the industry skip this step, thinking “more wire is just cheaper” but nah—tension is the backbone of the whole structure.
Let’s start with what happens when tension’s too low. Think of a slack shoelace: it bunch up, right? Well, low-tension wedge wires have that same floppy vibe. When your screen’s installed in a rotary drum, or vibrating screen, or even submerged in a wastewater tank, those loose wires will move under pressure. Every time material slams into them, or the screen vibrates, the wires bend and flex at the weld point. Over time, metal gets tired—this is called “fatigue cracking.” I’ve seen screens where half the welds split because someone cranked out production fast and skipped the tensioning step. Worse, those loose wires can shift, messing up your slot size. If a wedge wire moves 0.5mm out of place, suddenly you’re letting contaminants through that you’re supposed to filter out. That’s a quality control nightmare. Last year, a food processing client came to us because their old screen (from a no-name supplier) had low tension, and they were finding plastic particles in their finished syrup—cost them a $12k rework fee and a brand hit. The fix? We re-cut their screen with properly tensioned wires, and they haven’t had that issue since.
Now, what if tension’s too high? Wait, that’s not a good thing either. You ever overstretch a rubber band and it snaps instantly? Same idea here, though it’s a bit more nuanced. When you pull a wedge wire so tight that it’s at or near its yield strength (the point where metal stops bouncing back and stays deformed), you’re setting it up to snap under unexpected stress. Let’s say you have a screen processing gravel, and a big chunk of rock falls onto it. If the wire was stretched to its limit, that impact will make it snap right where it’s tensioned—way before it would have if it had a little give. Also, over-tensioned wires can warp the entire screen panel. I’ve had a mining client say their first order from a competitor had wires so tight that the whole panel curved inward, so material wouldn’t flow evenly across the screen surface. They had to weld extra support rods just to keep it straight, which wasted their time and money. That’s why we always test tension using a tensiometer—we target 60-70% of the wire’s tensile strength, the sweet spot where it’s tight enough to hold its shape but has room to flex when stressed.
Wait, let’s get into the science that actually backs this up, no fluff here. Tension directly affects three big factors that make up structural integrity: weld strength, wire deflection, and overall panel rigidity. Let’s go one by one. First, welds: when a wire is tensioned, it’s pulled straight before welding. That means when you attach it to the support rod, the weld is under constant, even pull, not like a slack wire where the weld has to hold a bunch of bending stress. We use TIG welding for our screens, and the process works way better when the wire’s straight—no gaps or uneven tension at the weld, so the bond is stronger. Tests we did last year (we don’t just guess, we have a little in-house lab) showed that tensioned wires have 30% stronger welds than non-tensioned ones. That’s a big number.
Next, wire deflection. Deflection is how much a wire bends under load. If your wire’s tensioned, it has higher stiffness, so it barely bends at all when pressure hits. No bending means no fatigue, no cracking, no shifting slots. If it’s too tight, deflection is low but so is the wire’s “yield margin,” so a random impact breaks it. If it’s too loose, deflection is high—like a slinky, it bounces a ton, wears out fast. We calculate deflection for every screen we make, based on the application. For example, a wastewater screen that’s submerged 24/7 has slightly higher tension than a food-grade screen that’s vibrated only 8 hours a day—makes sense, right? The wastewater screen has to handle constant hydrostatic pressure, so a little extra tension keeps it stable.
Then there’s overall panel rigidity. A properly tensioned set of wedge wires works like a truss—each wire pulls on the next, so the whole panel is stiffer, not just individual wires. Think of a fence: if all the rails are tight, the fence holds up. If they’re slack, it leans. Same exact principle. Last month, a chemical processing client brought us a screen that had cracked along the support rods after 3 months of use. Turns out the supplier they used cranked out the wires at low tension, so the entire panel was flexing with every pump pulse, stressing the support rods until they broke. We replaced it with a tensioned screen, and 2 months later they texted me saying it’s still running like new, no issues.
Wait, let’s address a common myth I hear all the time: “Wedge wire screens are all the same, right? Metal’s metal.” Nah, that’s like saying all cars are the same because they have four wheels. Tension is part of the custom engineering for your application, not a one-size-fits-all thing. For example, a screen used in paper pulp processing needs to handle heavy, abrasive material, so we use higher tension (around 70% of tensile strength) with thicker wedge wires. A screen for pharmaceutical filtration, which needs super precise slot sizes and no contamination, needs lower tension (around 60%) because even a tiny bit of deformation from over-tensioning could mess up the slot gap, leading to product waste.
I also want to mention something that a lot of suppliers cut corners on: tension consistency across the entire screen. If you tension the first wire super tight, the second a little loose, the third just right, you get uneven performance. That’s why we use computer-controlled tensioning machines, not manual pulls (I know some small suppliers still do that). Manual tensioning is hit-or-miss—one guy might pull 50lbs, another 70lbs, so you end up with a screen that’s half good, half garbage. Our machines pull every wedge wire to within 2% of our target tension, so every inch of the screen performs the same. That’s why our screens have a 5-year warranty, which is unheard of in this industry—we stand behind that consistency.
Let’s talk about real-world failure cases, because that’s where it hits home. Last year, a construction company reached out to us because their 3-month-old aggregate screen was full of broken wires. The supplier they bought from told them “vibration causes tension loss, so we make it extra tight to compensate.” Wait, that’s the opposite of what you should do! If you over-tension, you get instant failure from impact, not gradual tension loss. Their screen was using wires stretched to 95% of tensile strength—so when the vibration from the crusher ran, the wires snapped within days. We re-made their screen with proper tension (65%) and a little extra support rods to handle the vibration, and that screen’s been running for 10 months now. They told us it cuts their downtime by 40% compared to their old setup.
Another example: a water treatment plant that was replacing their wedge wire screens every 6 months. They were buying from a big supplier that used low-tension wires to keep costs down. We tested their old screens and found that the tension was only 30% of the wire’s tensile strength—no wonder they were failing! Loose wires were shifting, slots were getting too big, and the welds were splitting. We swapped them for our tensioned screens, and now they go 2.5 years between replacements. That’s a huge cost save for them—they don’t have to shut down the plant to replace screens every 6 months, which saves hundreds of thousands of dollars a year.
Now, let’s get back to the “why” behind the science, so you don’t just take my word for it. Wedge wires are typically made from stainless steel (304, 316, sometimes duplex for harsh chemicals) or even high-grade carbon steel for heavy abrasion. Every metal has a stress-strain curve—when you pull it, it stretches, and up to a point, it goes back to its original shape. That’s elastic deformation. Once you pass that yield point, it stays stretched (plastic deformation) and eventually breaks at the tensile strength. The sweet spot for tension is in the upper part of the elastic zone, right before yield. That’s where the wire is tight, stiff, and can absorb small impacts without deforming or breaking. If you stay in the elastic zone, the wire will go back to its original shape every time—no permanent bending, no fatigue cracks. That’s the key to structural integrity.
Wait, I should also mention a common mistake when installing screens: not accounting for tension during setup. Even if you have a perfectly tensioned screen, if you clamp it too tight when mounting it to the frame, you’re adding extra tension on the ends of the wires. That can make the wires go past their yield point on the edges, leading to early failure. We always include installation guides with every screen that tell our clients how to clamp it evenly, using spacers to keep tension consistent across the whole panel. We also have a team of techs that will walk you through installation for free—no extra charge.
Look, I’ve been doing this long enough to know that most clients don’t care about the physics as much as they care about not having downtime, not having contaminated product, and not wasting money on screens that last 2 months. The tension of wedge wires isn’t some trivial detail—it’s the thing that turns a pile of metal wires into a structural screen that works for years, not weeks. Too low, and you get shifting slots, weld failures, short lifespan. Too high, and you get instant snap failures, warped panels, wasted material. The sweet spot, tailored to your specific application, is where the magic happens.
If you’re tired of replacing wedge wire screens every few months, or dealing with product contamination or downtime from failed screens, let’s chat. We don’t do one-size-fits-all—we will engineer a screen with the right tension for your exact process, whether you’re in food and beverage, mining, wastewater, pharmaceuticals, or any other industry that uses filtration. Don’t waste another dollar on a screen that’s made with cheap, inconsistent tension. Hit us up to talk through your needs, and we’ll get you a custom solution that lasts.
Sintered Metal Material and Filter Element References:
- ASTM International. (2019). Standard Test Method for Tension Testing of Metallic Materials. ASTM E8/E8M-19a.
- Wedge Wire Filter Screen Manufacturing: Design, Performance, and Application Guidelines. (2021). Filter Media Industry Association.
- Metal Fatigue in Structural Filtration Components. (2020). Journal of Industrial Filtration and Separation Technology, Vol. 12, No. 2.
- Tension Effects on Weld Integrity of Wedge Wire Assemblies. (2018). Proceedings of the International Conference on Filtration and Separation.
Henan Easy Filter Equipment Co., Ltd.
As one of the leading wedge wire filter screen manufacturers and suppliers in China, we offer a wide range of products with superior quality. Please rest assured to buy advanced wedge wire filter screen from our factory. We also accept customized orders.
Address: Apartment No.1, Building No.2, Zhengshang Jinyushijia, Xinzhong Street, Xinxiang, Henan, China.
E-mail: vivian@easyfiltertech.com
WebSite: https://www.easyfilter-china.com/
