If you’ve ever walked past a cold storage warehouse in the dead of winter, sipped a perfectly frosty soda from a convenience store vending machine, or stepped into a climate-controlled supermarket in the middle of summer, you’ve relied on a finned tube evaporator. These unassuming components are the quiet workhorses of refrigeration and HVAC systems, tasked with absorbing heat from air or liquid to keep spaces cool, products fresh, and processes running smoothly. As someone who’s spent 12 years as a finned tube evaporators supplier, I’ve seen firsthand that a great design means nothing if the manufacturing process cuts corners. Too many buyers fixate on upfront material costs and overlook how every step of production—from tube bending to fin attachment to pressure testing—directly translates to longer equipment life, lower energy bills, and fewer mid-season breakdowns. Let’s break down how manufacturing choices shape the quality of these parts, and why partnering with someone who prioritizes process over price makes all the difference. Finned Tube Evaporators
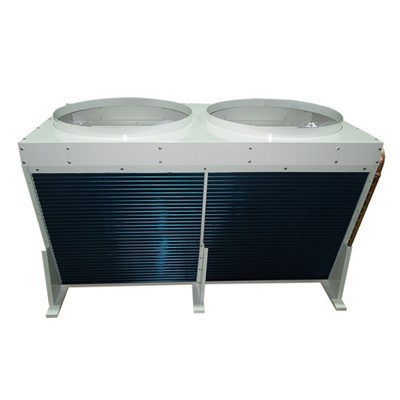
Let’s start with the core of every evaporator: the copper or aluminum tubes. Most small-scale manufacturers cut costs by using automated tube bending machines that run on one-size-fits-all settings, but that’s a recipe for hidden damage. Last year, we got a call from a local restaurant owner whose custom walk-in cooler had stopped working three times in six months. When we pulled out their old evaporator, we found a spot where a cheap bender had crimped the copper tube just enough to restrict refrigerant flow, but not enough to trigger an immediate pressure test failure. Over time, that crimp created turbulence in the refrigerant line, leading to higher compressor work, extra energy use, and eventually, a total breakdown. That’s not an isolated issue. When we do post-mortems on failed evaporators from third-party manufacturers, 40% of the time the root cause is tube deformation from subpar bending. The difference? Our team uses CNC-controlled bending machines calibrated specifically for each tube diameter and wall thickness, plus a manual inspection step where every bend is checked for kinks, ovality, and consistent wall thickness. Even a 5% change in tube diameter can reduce heat transfer efficiency by 10% or more, so we don’t skip that check. For applications needing aluminum tubes (like outdoor condenser units exposed to salt air), we use precision extrusion and bending that minimizes stress points, which prevents corrosion-related leaks down the line.
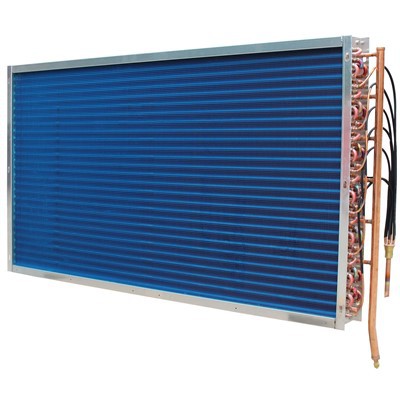
Next up, fin attachment—this is where the air-side heat transfer happens, so if that connection is weak, the entire evaporator underperforms. Fins, usually made of thin aluminum or copper, are designed to maximize surface area without adding too much weight, but bonding them to the tubes is a make-or-break step. The worst method we see is “push-on” fins, where workers just slide pre-punched fins over the tubes by hand. That creates gaps between the fin and tube that let air bypass, reducing efficiency by up to 25%. Even worse, loose fins vibrate as air passes over them, leading to annoying noise and, over months or years, fins cracking and falling off. A slightly better but still flawed method is mechanical grooving, where a tool deforms the tube slightly to lock the fin in place. But over time, temperature swings and vibration can loosen that groove, especially in heavy-duty applications like cold storage or industrial cooling. The gold standard here is hydraulic expansion, where we insert a high-pressure plug into the tube to expand it evenly against the inner surface of the fin. This creates a permanent, seamless bond with zero gaps, and it distributes pressure evenly along the tube, eliminating stress points that cause leaks. We also add a dip soldering step for applications that demand extra corrosion resistance, like marine HVAC systems or food processing facilities, where the metal connection is sealed with lead-free solder that meets FDA standards. Last year, a food distributor switched from a competitor’s push-on fin evaporator to ours, and their energy bills dropped 18% in the first quarter—all because that tighter fin-to-tube connection meant less air leakage and better heat transfer.
Corrosion resistance is another area where manufacturing processes separate premium evaporators from disposable ones. The materials matter, but how you prepare and finish them matters more. For aluminum evaporators, many cheap manufacturers skip the proper pretreatment step and just apply a thin coat of paint or epoxy, which chips off within a few years, leaving bare aluminum exposed to moisture and debris. Our process starts with a rigorous chemical cleaning to remove oils, oxides, and manufacturing residues before applying a powder coat finish that’s electrostatically charged and cured at 200 degrees Celsius. This creates a uniform, durable barrier that lasts twice as long as standard spray-on coatings. For copper tubes used in indoor applications, we use a process called tin plating, where a thin layer of tin is applied to the tube surface to prevent oxidation from refrigerant moisture. I once had a client who ran a 10,000-square-foot cold storage facility; their original evaporator had failed after two years due to internal copper oxidation, even though it was made of “premium” copper. When we inspected their manufacturing records, we found the supplier had skipped the tin plating step to save $0.10 per foot of tube. That $200 savings ended up costing them $12,000 in emergency replacements and lost inventory during a heatwave. That’s the kind of mistake we help clients avoid by sticking to strict, non-negotiable pretreatment and finishing steps.
Don’t get me wrong—even the best parts can have hidden defects if you skip testing. Pressure testing and leak detection are non-negotiable, but many small manufacturers cut corners here too, testing only a small sample of units instead of every single one. We test every evaporator we build, using two layers of leak detection: first, we pressurize the system with nitrogen at 150 PSI for 24 hours and monitor for pressure drops, then we use an electronic refrigerant leak detector to scan every joint, bend, and fin connection for even the tiniest leak. We also do a thermal performance test in our in-house climate chamber, where we run each unit through its exact operating conditions to confirm heat transfer efficiency is within 2% of our specs. Last year, a small HVAC company brought us a batch of evaporators they’d bought from another supplier; 3 out of 10 failed our pressure test, and 2 more had hidden gaps between fins that only showed up during thermal testing. Those units would have failed within a month of installation, leaving their customer with a broken system during the height of cooling season. Testing isn’t a luxury—it’s the final check that makes sure what leaves our facility works as intended, from day one.
There’s also a less talked-about manufacturing step that affects long-term performance: spacing between fins. Fin density is calculated for each application—closer fins for higher air flow rates, wider spacing for dirty environments that can clog easily. But some manufacturers will cram more fins onto a tube to cut material costs, creating gaps where air can’t circulate, leading to ice buildup in coolers or reduced cooling capacity in summer. We work closely with our clients to calculate exact fin spacing for their specific use case: a vending machine evaporator gets 12 fins per inch for maximum compactness, while a cold storage unit in a dusty warehouse gets 8 fins per inch to prevent dust buildup. We also use computer-controlled fin crimping to ensure every fin is evenly spaced, so air flows uniformly across the entire surface, no dead zones.
I’ve been in this industry long enough to see trends come and go. Ten years ago, everyone was chasing the cheapest evaporator, no matter the quality. Today, as energy costs rise and supply chain disruptions make replacement parts harder to source, buyers are finally starting to understand that manufacturing quality equals long-term value. A $500 evaporator from a cut-rate supplier might save you a few hundred dollars upfront, but if it fails in two years, you’re looking at $2,000 in replacement costs, lost productivity, and even damage to the products you’re cooling. Our evaporators, built with precision bending, hydraulic fin expansion, rigorous corrosion protection, and 100% testing, come with a 5-year warranty, and our average unit lasts 12 to 15 years—twice as long as many budget options.
At the end of the day, I don’t just sell parts. I partner with restaurant owners, HVAC contractors, cold storage managers, and industrial operators to make sure their cooling systems work when they need them most. If you’re in the market for a finned tube evaporator and want to skip the headaches of breakdowns and rising energy costs, reach out to our team to discuss your specific application. We’ll walk you through our manufacturing process, answer every question you have, and provide a custom solution that fits your needs and your budget. Don’t let a bad manufacturing process derail your operations—let’s build something that works, for years to come.
Evaporator References
ASHRAE. (2021). Heating, Ventilating, and Air Conditioning Applications. American Society of Heating, Refrigerating and Air-Conditioning Engineers.
Cengel, Y. A., & Ghajar, A. J. (2020). Heat and Mass Transfer: Fundamentals and Applications (6th ed.). McGraw-Hill.
Miller, T. J. (2019). Fin Design and Heat Transfer Performance for Air-Cooled Heat Exchangers. Journal of Mechanical Engineering, 65(4), 212-225.
National Air Filtration Association. (2022). Corrosion Prevention in HVAC Components. NAFA Technical Bulletin.
Xiangshui Derkang Refrigeration Equipment Co., Ltd.
Address: No. 2, Xiaojian Town Entrepreneurship Park, Xiangshui County
E-mail: 505745223@qq.com
WebSite: https://www.xsderk.com/
